Smartwatches and modern watches are looking for small size, durability, accuracy and aesthetics in custom metal injection molded watch components. In addition, many of these parts are complex in shape, which can be challenging to manufacture using conventional machining processes. Metal Injection Molding (MIM) is a viable manufacturing process for complex metal components that can be produced in volume. In addition to traditional watches and wearable devices, the process of custom Metal Injection Molded Watch Parts can be adapted to specific dimensions, materials, tolerances and finishing.
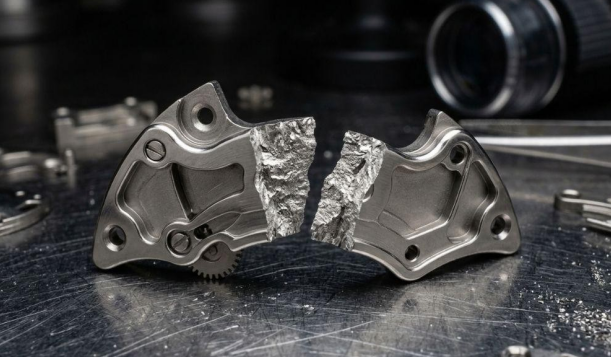
Custom MIM watch components are metal components that are manufactured using the Metal Injection Molding (MIM) process, which are designed to meet the requirements of a particular metal watch product. Custom parts are not just the standard parts that are available off the shelf; they are specifically designed to fit the watch manufacturer's needs. The process involves the preparation of fine metal powder, adding a binder to the powder, molding the material in a mold, eliminating the binder, and finally sintering the molded part to obtain the desired metal
properties. This is particularly beneficial for small components that have complex geometries, critical tolerances, and require frequent manufacturing.
The components can be made using MIM for numerous small-scale watch and smartwatch components. The specific application will vary by component design, material, size, tolerance and volume of production.
The shapes and clean surface of watch frames, cases and back covers can be intricate. These components can be moulded close to their final shape, thus minimizing machining required after the moulding process. It can also be used for design details like curves, openings, grooves, etc.
Such components as crowns, pushers, buttons and others require precise dimensions because they should fit well with the other watch parts. These small parts can be manufactured consistently by MIM and enable the manufacturers to choose the appropriate metals and surface finishes for the desired surface finish.
Small connectors, clasps, hinges, locking members and adapters are common on watch straps. These components must be strong and have reliable dimensions to assemble and use every day. MIM is ideal for making multiple quantities of small, complex metal components.
There are numerous small components within smartwatches that need to fit into a compact area. The MIM can be used for internal connectors, brackets, supports and structural inserts. An ability to create complex shapes makes it possible for manufacturers to incorporate several features together into a smaller metal part.
The MIM process consists of various controlled steps and the quality of each stage influences the quality of the final product.
1. Feedstock preparation: Feedstock is prepared by mixing fine metal powder with an appropriate binder system that enables feedstock to flow during injection molding.
2. Injection molding: Feedstock is heated and pushed into a form that is already made. The mold sets the general outline and details of the watch part.
3. Debinding: The binder is slowly drained out of the part after molding. This stage is very critical and needs to be closely monitored to avoid defect.
4. Sintering: The debound part is put into a furnace and heated at a controlled temperature. The remaining binder is burned off and the desired density and strength are obtained as the metal particles fuse together.
5. Finishing: The component can be polished, machined, coated, plated or finished in another way according to its application.
The material depends upon the strength, weight, corrosion resistance, appearance and operating conditions required. One of the popular choices is stainless steel, as it is durable and has a good level of corrosion resistance. Surface appearance and corrosion resistance are important, and 316L stainless steel can be used, 304 stainless steel can be used for selected hardware applications. When greater strength is needed, 17-4PH stainless steel should be considered. In situations where low weight and strength is paramount, titanium and other suitable alloys may be used.
The selection of material should be made for the intended use of the component rather than just for looks. The manufacturer should also take into account the finishing process and the performance that is required after the process.
The surface finish may significantly affect the look and feel of a watch part. The surface finish on the visible parts may require a smooth and high quality surface while surface finish of the
non-visible parts may be less critical.
These methods include polishing, brushing or wire drawing, sand-blasting, plating and PVD coating. A smooth and reflective surface can be achieved by polishing, and a controlled directional texture can be achieved by brushing. Smooth out matte finish with sand blaster.
Decorative aspects or other surface properties can be achieved by plating or PVD coatings. The choice of finishing will depend upon the design of the component, its location, the wear it is likely to endure, the material it is constructed from and the appearance desired.
Manufacturers may want to consider MIM for watch components for a number of reasons. Firstly, it can create small, intricate and three dimensional objects with the same shape over and
over. It can also eliminate the need for multiple machining processes, which could allow for multiple features to be formed in the mold.
If the parts are required in higher quantity, MIM can deliver consistent parts after developing the right tooling and process. It also is compatible with a variety of metal materials and finishes.
Therefore, Custom Metal Injection Molded Watch Components can assist manufacturers in striking the right balance between intricate designs, manufacturing consistency, and efficiency.
But not every part of a watch is appropriate to use MIM. Simple components, very low production volumes or designs that are not conducive to injection molding may be better produced by another method.
While both MIM and CNC have their own significance in the watch-making industry, they function differently.
Factor | Metal Injection Molding | CNC Machining |
Complex shapes - | Highly suitable for many small complex parts | Suitable, but complex parts may require several operations |
Production volume - | Well suited to repeat and higher-volume production | Flexible for low to medium volumes |
Material waste - | Generally lower for near-net-shape production | More material is removed during machining |
Tooling - | Requires dedicated molds | Uses machining tools and fixtures |
Small components - | Well suited to many small parts | Also suitable, depending on geometry |
Design flexibility - | Best for designs that suit molding | Broad flexibility for machined geometries |
The design is the key factor prior to production. The size, wall thickness, weight, tolerances, openings, and the complexity of a component are all factors that need to be taken into account by engineers. They also must consider changes in material behavior and dimensional changes during debinding and sintering.
Another design aspect is mold design. The quality of the production can be influenced by location of the gate, parting lines, draft requirements, etc., and by the placement of features. The designers should also determine if there are any sections that will need secondary molding after the molding process. The ability to review design in 2D drawings and accurate 3D CAD models simplifies the design evaluation process before the start of tooling.
For watches, uniformity of dimensions is often critical, as only slight differences can impact assembly. The material, molding process, dimensional accuracy, surface appearance and final part performance should therefore be covered by the quality control.
Dimensional inspection, visual surface inspection, material checks, density measurements or functional and assembly testing may be used by manufacturers. There may also be additional inspections to make of critical components depending on the customer's requirements.
Maintains process control and minimises the variation between production runs, enabling reliable final assembly.
If the watch component is small, detailed, complex and is needed in multiple quantities, M
Save money - with manufacturer direct pricing
Save time - with experienced team to get project done
Lead the industry - with the most cutting-edge products
 Send A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
 English